Introduction to Conveying Diverter Valve
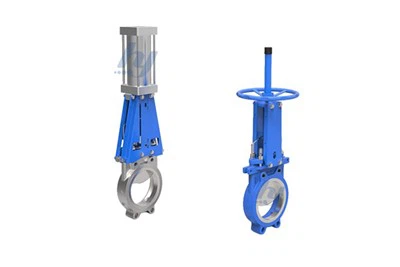
A conveying diverter valve is a crucial component in pneumatic conveying systems and bulk material handling processes. It is designed to direct the flow of materials, such as powders, granules, and pellets, from one conveying line to another. These valves play a vital role in ensuring efficient and reliable material transfer in industries like food processing, pharmaceuticals, chemical, and plastics manufacturing. They need to be durable, precise, and capable of handling different types of materials and operating conditions. Conveying Diverter Valve
Top 10 Manufacturers
1. Shanghai Hanye Engineering Technology Co., Ltd.
Shanghai Hanye Engineering Technology Co., Ltd. is a leading company focusing on pneumatic conveying systems and relevant equipment. With years of experience and a professional R & D team, the company has a deep understanding of the needs of various industries in material handling.
Features in Conveying Diverter Valve
- High – Quality Materials: Utilize high – performance alloys and engineering plastics in the production of valves, ensuring high wear resistance and long service life, especially suitable for handling abrasive materials.
- Precise Design: The valve design allows for accurate control of material flow direction, minimizing the retention of materials in the valve cavity and reducing the risk of blockage.
- Customization: Can provide customized diverter valves according to the specific process requirements of customers, including different connection sizes, materials, and operating temperatures.
Advantages
- Cost – effective: Offer products with competitive prices while maintaining high quality, helping customers to reduce overall investment in material handling systems.
- Excellent After – sales Service: Have a professional after – sales team that can quickly respond to customer problems and provide on – site maintenance and technical support.
- Rich Project Experience: Have successfully completed a large number of material handling projects in different industries, which can provide reference and solution for new customers.
Website
2. Spiroflow Systems
Spiroflow Systems is a well – known global leader in bulk material handling. Founded several decades ago, it has established a solid reputation in the industry. The company has a wide range of products and services, covering from simple conveying solutions to complete turn – key systems.
Features in Conveying Diverter Valve
- Versatile Design: Their diverter valves can handle a wide variety of materials, from fine powders to large particles, and can adapt to different pressures and flow rates in the conveying process.
- Sanitary Design: In industries such as food and pharmaceuticals, Spiroflow’s valves are designed with strict sanitary standards, featuring smooth surfaces and easy – to – clean structures to prevent cross – contamination.
- Integrated Solutions: The company can integrate diverter valves into a complete material handling system, ensuring seamless operation and high – efficiency flow control.
Advantages
- Global Network: With offices and service centers around the world, they can provide quick and efficient support to customers no matter where they are located.
- Innovative Technology: Continuously invest in research and development to introduce new technologies and improve the performance of their diverter valves, such as using advanced sensors for real – time monitoring.
- Industry Expertise: Have in – depth knowledge of different industries’ requirements, which allows them to provide optimized solutions for specific applications.
3. Flexicon Corporation
Flexicon is a pioneer in the field of flexible screw conveyors and bulk material handling equipment. The company has been dedicated to developing innovative and reliable solutions for material transfer for many years.
Features in Conveying Diverter Valve
- Gentle Material Handling: Their diverter valves are designed to handle materials gently, minimizing particle degradation, which is crucial for materials like fragile granules and fibers.
- Easy Maintenance: The valve structure is designed for easy disassembly and cleaning, reducing downtime for maintenance and improving overall equipment utilization.
- High – Speed Operation: Capable of handling high – speed material flow, which meets the requirements of high – throughput production lines.
Advantages
- Proven Track Record: Have a long – standing history of providing high – quality equipment to various industries, which gives customers confidence in the reliability of their products.
- Customer – centric Approach: Focus on understanding customer needs and providing personalized service, from product selection to system installation and commissioning.
- Technical Support: Offer comprehensive technical support, including training for customers’ operators to ensure proper operation and maintenance of the diverter valves.
4. Schenck Process
Schenck Process is a global player in industrial weighing and feeding technology, as well as bulk material handling. The company has a strong R & D and manufacturing base, and its products are widely used in industries such as mining, cement, and chemicals.
Features in Conveying Diverter Valve
- Robust Construction: Built with heavy – duty materials to withstand harsh industrial environments, such as high temperatures, high pressures, and corrosive substances.
- Accurate Flow Control: Equipped with advanced control systems to ensure accurate and stable material flow diversion, which is essential for continuous and stable production processes.
- Compatibility: Their diverter valves can be easily integrated with other Schenck Process equipment, such as feeders and conveyors, forming a unified and efficient material handling system.
Advantages
- System Integration Capability: With strong system integration capabilities, they can design and implement large – scale material handling systems, providing one – stop solutions for customers.
- Quality Assurance: Comply with strict international quality standards, ensuring the high quality and reliability of their products through rigorous testing and inspection procedures.
- Long – term Partnership: Have established long – term partnerships with many well – known companies around the world, which reflects their high – level service and product quality.
5. Endress+Hauser
Endress+Hauser is a well – respected manufacturer in the field of measurement and automation technology. The company offers a wide range of products for process industries, including sensors, controllers, and valves.
Features in Conveying Diverter Valve
- Intelligent Control: Their diverter valves are often equipped with intelligent sensors and control systems, allowing for real – time monitoring of valve status, position, and material flow. This enables predictive maintenance and optimized process control.
- High – Precision Manufacturing: Use advanced manufacturing technology to ensure high – precision valve components, which results in accurate and reliable material diversion.
- Corrosion Resistance: Suitable for handling corrosive materials, as the valves can be made of corrosion – resistant materials such as stainless steel and special alloys.
Advantages
- Leading Technology: Always at the forefront of technological innovation, which enables them to provide state – of – the – art diverter valves with high performance and advanced features.
- Comprehensive Product Portfolio: In addition to diverter valves, they offer a full range of measurement and control products, which can be integrated to provide a complete solution for material handling processes.
- Global Customer Service: With a global customer service network, they can quickly respond to customer needs and provide technical support and maintenance services.
6. Coperion GmbH
Coperion is a leading provider of compounding and extrusion systems, as well as bulk material handling solutions. The company has a long – term focus on the plastics and chemical industries, with in – depth expertise in these fields.
Features in Conveying Diverter Valve
- High – Pressure Resistance: Their diverter valves are designed to withstand high – pressure pneumatic conveying systems, which are common in the plastics and chemical industries for efficient material transfer.
- Precise Material Separation: Capable of accurately separating different materials during the conveying process, which is important for multi – component material handling in these industries.
- Compact Design: The valve design is compact, saving space in the production line and allowing for easy installation in limited – space environments.
Advantages
- Industry – specific Solutions: Have in – depth knowledge of the plastics and chemical industries, and can provide customized diverter valves and solutions according to the unique requirements of these industries.
- Reliable Performance: Their products are known for their reliable performance, which helps to reduce production downtime and improve overall production efficiency.
- Continuous Innovation: Continuously invest in research and development to improve the performance and functionality of their diverter valves, keeping up with the development of the industry.
7. Gericke Group
Gericke is a family – owned company with a long history in the field of powder and bulk solids handling. The company has a global presence and offers a wide range of equipment and systems for various industries.
Features in Conveying Diverter Valve
- Low – Maintenance Design: The valve structure is designed to minimize the need for maintenance, with features such as self – cleaning functions and long – lasting seals.
- Hygienic Design Options: For industries with strict hygiene requirements, such as food and pharmaceuticals, Gericke offers diverter valves with hygienic features, including smooth surfaces and easy – to – disassemble parts for cleaning.
- High – Flow Capacity: Can handle large – volume material flow, meeting the high – throughput requirements of modern production lines.
Advantages
- Family – Business Values: As a family – owned company, Gericke emphasizes long – term relationships with customers, providing personalized service and support.
- Global Distribution Network: With a wide – spread distribution network, they can quickly deliver products to customers around the world and provide local after – sales service.
- Technical Know – how: Have comprehensive technical know – how in powder and bulk solids handling, which allows them to develop high – performance diverter valves.
8. AZO GmbH & Co. KG
AZO is a specialist in automation and process technology for the food, chemical, and pharmaceutical industries. The company focuses on providing integrated solutions for material handling, storage, and dosing.
Features in Conveying Diverter Valve
- Automation Compatibility: Their diverter valves are highly compatible with automation systems, allowing for seamless integration into fully automated production lines. This enables remote control and monitoring of valve operations.
- Material – Specific Design: Can design diverter valves according to the specific properties of the conveyed materials, such as hygroscopic powders or sticky substances, to ensure smooth and reliable material flow.
- Safety – Oriented Design: Incorporate safety features in the valve design, such as safety interlocks and explosion – proof options, to meet the safety requirements of different industries.
Advantages
- Automation Expertise: With extensive experience in automation technology, they can provide turn – key solutions for automated material handling systems with diverter valves at the core.
- Regulatory Compliance: Ensure that their products comply with relevant industry regulations and standards, providing customers with legal and reliable products.
- System Optimization: Analyze the entire production process and optimize the design and installation of diverter valves to improve the overall efficiency and productivity of the system.
9. Pelletron Corporation
Pelletron is a leading manufacturer of pneumatic conveying systems, rotary valves, and other bulk material handling equipment. The company has a reputation for providing high – quality products and excellent customer service.
Features in Conveying Diverter Valve
- High – Speed Rotating Parts: Their diverter valves may have high – speed rotating components, which can achieve rapid and efficient material diversion in high – speed conveying systems.
- Low – Leakage Design: Designed to minimize material leakage, ensuring that the conveyed materials are accurately directed to the desired destination and reducing material waste.
- Customizable Configurations: Offer a variety of customizable configurations, such as different valve body shapes and inlet/ outlet orientations, to meet the specific layout requirements of customers’ production lines.
Advantages
- Product Quality: Have a strict quality control system, ensuring that each diverter valve meets high – quality standards before leaving the factory.
- Quick Response: The company is known for its quick response to customer inquiries and orders, providing fast delivery and installation services.
- Technical Training: Provide technical training for customers’ operators, helping them to better understand and operate the diverter valves.
10. Zeppelin Systems GmbH
Zeppelin Systems is a global provider of turn – key solutions for bulk material handling in various industries, including energy, mining, and chemicals. The company has a strong engineering and manufacturing background.
Features in Conveying Diverter Valve
- Heavy – Duty Application: Their diverter valves are designed for heavy – duty applications, capable of handling large – size materials and high – volume material flow in harsh industrial environments.
- Integrated System Design: Can integrate diverter valves into a comprehensive material handling system, considering factors such as material flow balance, energy consumption, and equipment reliability.
- Long – Life Components: Use high – quality and long – life components in the valve manufacturing, reducing the frequency of component replacement and maintenance costs.

Advantages
- Project Management Experience: Have extensive experience in managing large – scale projects, from system design to installation and commissioning, ensuring the smooth implementation of projects.
- Global Competence Center: With a global competence center, they can share knowledge and experience across different regions and industries, providing best – practice solutions to customers.
- After – sales Service Network: Have a well – established after – sales service network, which can provide timely maintenance and spare parts replacement services to ensure the continuous operation of the diverter valves.
Sinter Plate Dust Collector In conclusion, these 10 manufacturers represent the top – level in the field of conveying diverter valves. Each of them has its own unique features and advantages, which can meet the diverse needs of different industries and customers in the process of material handling.
